© CyNex Systems, All rights reserved. 2024
Machine Vision and AI
You are here: Cynex.ca
Engineering & Design - Machine Vision and AI
Popular Services:
Cynex Systems
Engineering. Manufacturing. Automation.
One Idea. One vision.
Turning possibilities into performance.
>> Get In Touch
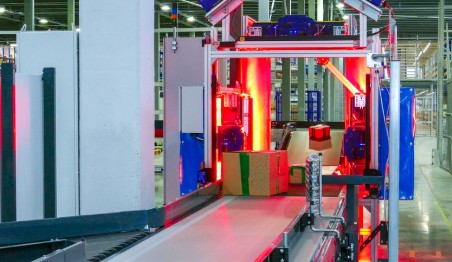
At Cynex Systems, machine vision and artificial intelligence combine visual perception, intelligent data processing, and automation to help machines interpret their surroundings, recognize objects, detect defects, and support operational decisions. Our engineering approach focuses on integrating cameras, image-processing technologies, AI algorithms, and control systems into practical solutions for agriculture, industrial manufacturing, warehousing, logistics, and robotics.
Engineering & Design Capabilities
Our machine vision and AI engineering scope includes visual inspection, object recognition, image analysis, dimensional measurement, defect detection, product classification, and integration with industrial automation systems. By transforming images and sensor data into actionable information, these technologies can improve inspection consistency, reduce repetitive manual tasks, enhance traceability, and support more efficient operations.
Agriculture & Intelligent Farming
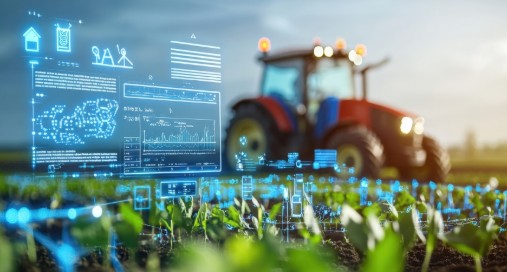
Machine vision and AI offer valuable opportunities to improve agricultural productivity and precision. Applications include crop monitoring, plant counting, fruit detection, produce grading, weed recognition, and identification of visible signs of disease or crop stress. Vision-guided agricultural machinery can support selective harvesting, robotic picking, targeted spraying, and automated sorting. In greenhouses, intelligent imaging can assist with plant-growth monitoring, crop assessment, and automated handling. When combined with suitable sensors, GPS, and agricultural control systems, these technologies can support more precise resource utilization and informed farm management. Reliable implementation requires consideration of changing lighting, dust, moisture, crop variability, and outdoor operating conditions.
Industrial Vision & Quality Inspection
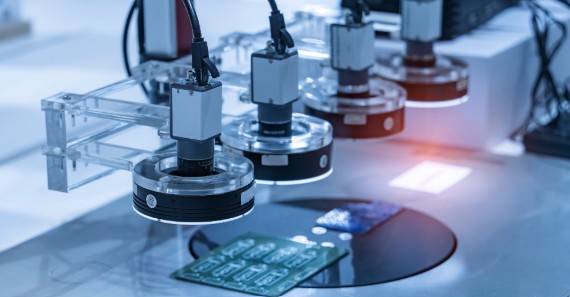
In manufacturing, machine vision enables automated product inspection, component verification, dimensional measurement, surface-defect detection, barcode reading, and assembly validation. AI-based inspection can identify complex defects and variations that may be difficult to detect using conventional image-processing techniques. Integrated with production equipment, vision systems can trigger alarms, sorting mechanisms, and quality-control actions. These applications support consistent inspection, improved product quality, reduced waste, and better production traceability. Performance depends on appropriate imaging hardware, representative training data, and validation under actual operating conditions.
Industrial Vision & Quality Inspection
In manufacturing, machine vision enables automated product inspection, component verification, dimensional measurement, surface-defect detection, barcode reading, and assembly validation. AI-based inspection can identify complex defects and variations that may be difficult to detect using conventional image-processing techniques. Integrated with production equipment, vision systems can trigger alarms, sorting mechanisms, and quality-control actions. These applications support consistent inspection, improved product quality, reduced waste, and better production traceability. Performance depends on appropriate imaging hardware, representative training data, and validation under actual operating conditions.
Warehouse Automation & Logistics
Machine vision and AI can improve warehouse operations through automated barcode reading, package identification, product counting, pallet inspection, parcel dimensioning, and intelligent sorting. Vision-guided robotic systems can identify objects, determine their positions, and support automated picking and placement. Integration with warehouse management systems, conveyors, and automated storage equipment can improve inventory visibility and material-flow coordination.
Robotics & Intelligent Automation
Vision and AI enhance robotic capabilities by enabling object recognition, part orientation, visual tracking, precision positioning, and adaptive handling. Applications include robotic assembly, pick-and-place operations, automated inspection, and intelligent material handling. Three-dimensional vision and depth sensing can provide additional spatial information for complex tasks. AI can also support anomaly detection and equipment monitoring. Safety-critical applications require appropriate protective systems and validated safety architectures.
System Integration & Performance
Depending on project requirements, engineering activities may include camera and lens selection, lighting design, image acquisition, AI model development or integration, software configuration, PLC connectivity, and system testing. Solutions can be evaluated using detection accuracy, processing speed, false-alarm rates, inspection coverage, and reliability under real operating conditions. Appropriate computing platforms, cybersecurity, maintainability, and data management are also important design considerations.
Enabling Smarter Operations
Machine vision and artificial intelligence create opportunities to improve quality, precision, productivity, and operational flexibility across agriculture, industry, and logistics. CYNEX Systems' engineering approach brings together intelligent perception, image analysis, and automation integration to support the development of smarter equipment and more adaptive industrial processes.
Cynex Systems — Seeing More. Understanding Better. Automating Smarter.
- Engineering
- Manufacturing
- Mechatronics
- AI and Machine Vision
- Automation And Robotics